Build the product side
Water quality, recipe, syrup handling, mixing, chilling and carbonation define what reaches the filler.
- Mixing basis
- Product temperature
- CO2 target
- Transfer and buffer pressure
Carbonated beverage projects depend on a controlled product-temperature and pressure route. Container preparation, carbonation, buffer transfer, filling, closure and downstream handling must be reviewed as one system.
A preliminary route may include treated water, syrup preparation, mixing, chilling, carbonation, product buffer, CIP, container preparation, isobaric filling, capping or seaming, inspection, labeling and packing.
Stable isobaric filling depends on the product delivered to the filler and on immediate closure and downstream handling.
| Selection gate | Confirm | Evidence |
|---|---|---|
| Product condition | Carbonation and filler-inlet temperature | Approved measurement method |
| Pressure path | Carbonator, buffer and filler requirements | Operating pressure/temperature window |
| Package | Bottle/can resistance and closure | Controlled drawings and samples |
| Post-fill route | Leak checks, warming, drying and packing | Finished-package condition plan |
A filling symptom can begin upstream or continue downstream. Record conditions during stable production and after stops before changing machine settings.
| Observed symptom | Interfaces to inspect | Evidence to capture | Do not assume |
|---|---|---|---|
| Excessive foam at filling | Product temperature, pressure, transfer, bowl and venting sequence | Time-stamped temperature/pressure trend and representative containers | The filler valve is the only cause |
| Variable fill or headspace | Product supply stability, container variation, fill control and restart state | Good/reject sample set linked to operating state | One static sample represents the run |
| CO₂ below target after closing | Carbonation measurement, transfer loss, venting, headspace and closure delay | Agreed measurement method before and after filling | A single instrument reading closes the cause |
| Losses after short stops | Buffer control, pressure equalization, restart recipe and first-off disposition | Stop duration, alarm sequence, settings and release record | Nameplate speed describes restart behavior |
| Wet or unstable downstream pack | Warming/drying, conveyor contact, label surface and packing pressure | Container condition at each equipment handoff | The issue remains inside the filler boundary |
Decision boundary: Final operating settings require trials with the approved beverage, container and closure. This matrix is a diagnostic evidence plan, not a universal recipe.
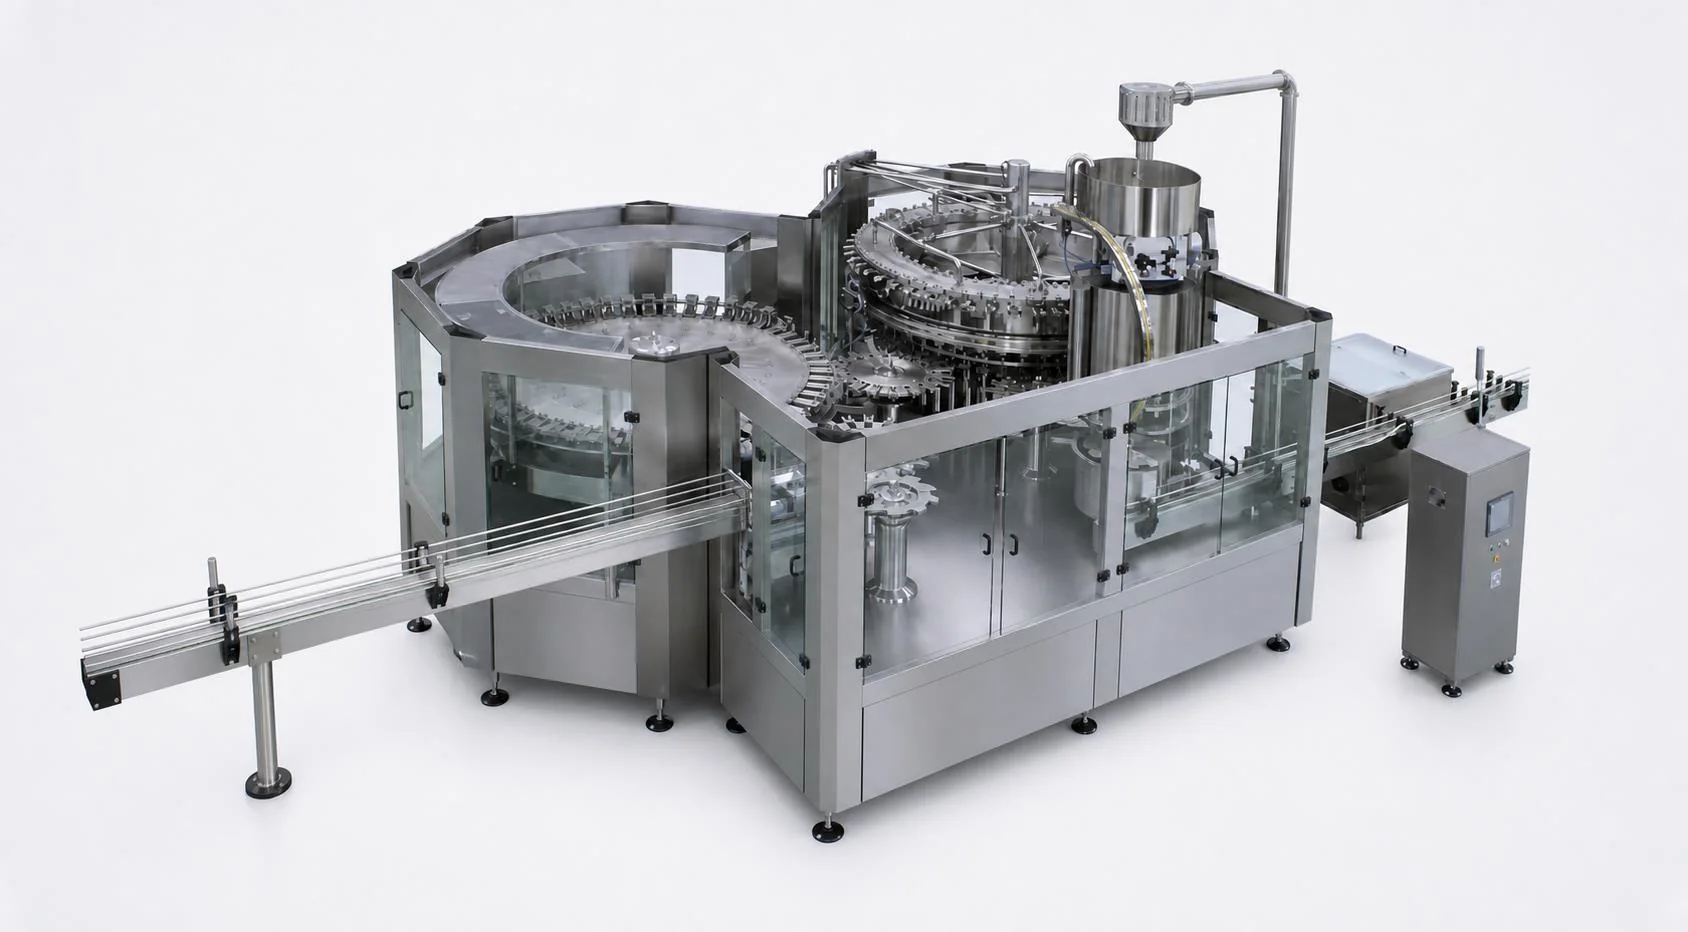
Water quality, recipe, syrup handling, mixing, chilling and carbonation define what reaches the filler.
PET bottles, glass bottles and cans have different pressure suitability, closure and handling requirements.
Transfer, filler inlet, filling method, closure timing and warm-up or downstream handling should be confirmed together.
Every equipment decision has an upstream condition, a current function and a downstream handoff.
Chilled, carbonated product and prepared container.
Pressure-controlled filling and immediate closing or seaming.
Inspect closure, stabilize container handling, label and pack.
The supplied Allot Tech 2026 catalog supports named equipment groups such as water treatment, beverage preparation, CIP, bottle handling, filling platforms, labeling, conveying and secondary packaging. It does not make every module mandatory for every project.
Company identity, contact route, named equipment categories and catalog reference flows.
Application routes and model-family context from the supplied catalog.
Output, power, dimensions, materials, components, process conditions, availability, price and service scope.
Invented performance, price, certifications, projects, reviews, factory claims or guarantees.
These answers frame the equipment decision. The final process and equipment remain project-specific.
It affects how readily dissolved CO2 leaves the beverage, so temperature, pressure and transfer conditions must be coordinated.
They may share product preparation, but container handling, filling, closing, conveying and packing equipment differ.