Separate new and returnable bottle routes
Returnable bottles introduce collection condition, sorting, external and internal washing, contamination checks and crate handling.
- Bottle history
- Washer scope
- Inspection points
- Crate and return logistics
New and returnable glass bottles need different preparation. Product condition, closure, breakage control, inspection and pack format determine the connected equipment scope.
The project must decide new versus returnable bottles, bottle inspection and washing requirements, filling method, crown or other closure, glass-safe conveying, reject handling and crate or carton packing.
Incoming bottle condition determines washing, inspection, breakage control and handling before the filling method is selected.
| Decision | Confirm | Evidence |
|---|---|---|
| Bottle source | New or returnable pool | Incoming-condition audit |
| Preparation | Rinse, wash and empty-bottle inspection | Cleaning and reject criteria |
| Filling and closure | Product condition and closure type | Bottle/closure trials |
| Handling | Pressure, thermal shock and breakage controls | Transfer and containment plan |
New one-way glass and a variable returnable pool create different washing, inspection, breakage and acceptance duties even when the beverage and filler are similar.
| Decision block | New one-way glass | Returnable glass | Evidence gate |
|---|---|---|---|
| Incoming condition | Supplier packaging, dust and transit damage | Soil, foreign objects, wear and mixed bottle population | Incoming audit and reject policy |
| Preparation | Depalletize/unpack and rinse as required | Sort, decap, wash and rinse under validated procedure | Approved cleaning and inspection route |
| Empty-bottle inspection | Damage and cleanliness criteria | Residual liquid, contamination and damage criteria | Defect library and challenge method |
| Filling/closure duty | Controlled bottle and closure variation | Pool variation plus repeated-use condition | Approved samples, tooling and handling trial |
| Breakage containment | Glass-safe transfer and cleanup plan | Additional pool-condition and washer/filler controls | Containment, line clearance and product disposition |
Decision boundary: Bottle washing or inspection cannot be specified from “glass” alone. Final criteria require the real bottle population and applicable quality requirements.
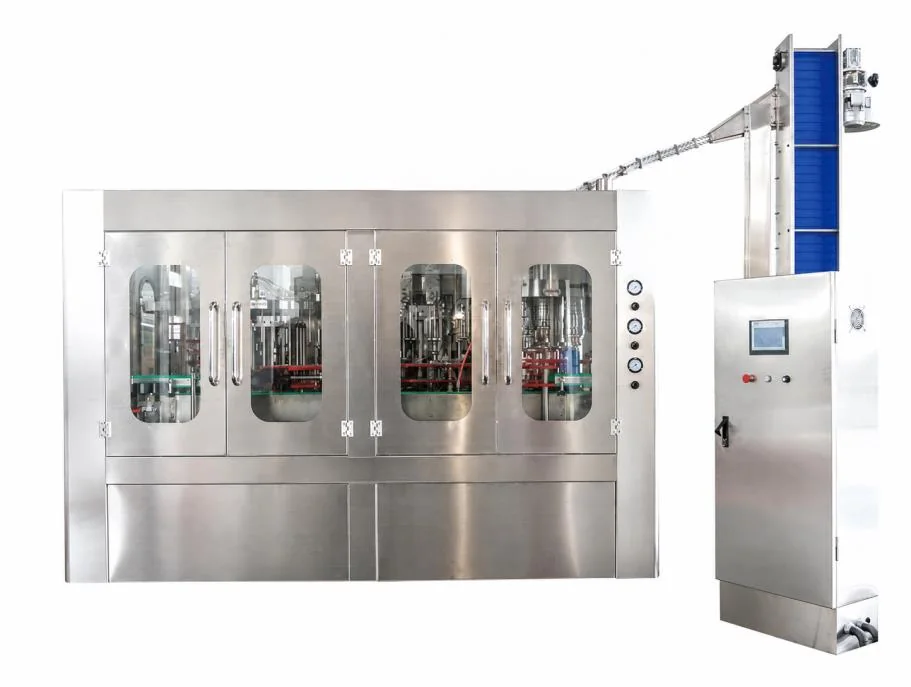
Returnable bottles introduce collection condition, sorting, external and internal washing, contamination checks and crate handling.
Still, carbonated, beer, juice and tea applications can require different filling conditions and closures.
Conveyor geometry, transfer, guarding, drainage, cleanup and reject routes should account for glass risk.
Every equipment decision has an upstream condition, a current function and a downstream handoff.
Received, inspected and cleaned glass containers plus prepared beverage.
Fill and close using the confirmed product and bottle route.
Inspect, convey safely, label and pack in cartons or crates.
The supplied Allot Tech 2026 catalog supports named equipment groups such as water treatment, beverage preparation, CIP, bottle handling, filling platforms, labeling, conveying and secondary packaging. It does not make every module mandatory for every project.
Company identity, contact route, named equipment categories and catalog reference flows.
Application routes and model-family context from the supplied catalog.
Output, power, dimensions, materials, components, process conditions, availability, price and service scope.
Invented performance, price, certifications, projects, reviews, factory claims or guarantees.
These answers frame the equipment decision. The final process and equipment remain project-specific.
Not as a general assumption. Container handling, filling, closure, protection and machine design must be confirmed.
Not necessarily. Incoming condition and the approved cleaning method define the preparation scope.